Undercuts
Undercuts, classified as internal and external are often required for part function.
Undercuts may increase tooling costs and lengthen cycles, but this is dependent on the type and location of the undercuts on the part.
External undercuts, often specified on MIM parts for ‘o’-ring seating can be formed by using a split cavity mould. As with the threaded components, there will be two parting lines 180° apart on the surface of the undercut, which may be objectionable in an ‘o’-ring groove.
Internal undercuts can be formed by using collapsible cores. However, most MIM parts are relatively small and cannot accommodate this approach. Designing MIM parts with internal undercuts or recesses is not recommended.
Tolerances
MIM processing normally requires a dimensional tolerance of +/-0.003 mm/mm (+/-0.3%).
As part size decreases, increasingly tighter tolerances can be achieved, as would be expected. However, the reduction in tolerances is not directly proportional to decreasing dimensions and may depend on material, part shape, and process requirements.
A tolerance of +/-0.001 mm/mm (+/-0.1%) can generally be held on a small, selected dimension when the mould has been ‘fine-tuned’
Surface Finish
Surface finish of MIM parts is approximately 0.80 µm, appreciably better than most investment castings. However, profilometer readings may be affected by residual porosity and are subject to interpretation.
The method of measuring surface finish should be agreed upon by both the customer and the vendor.
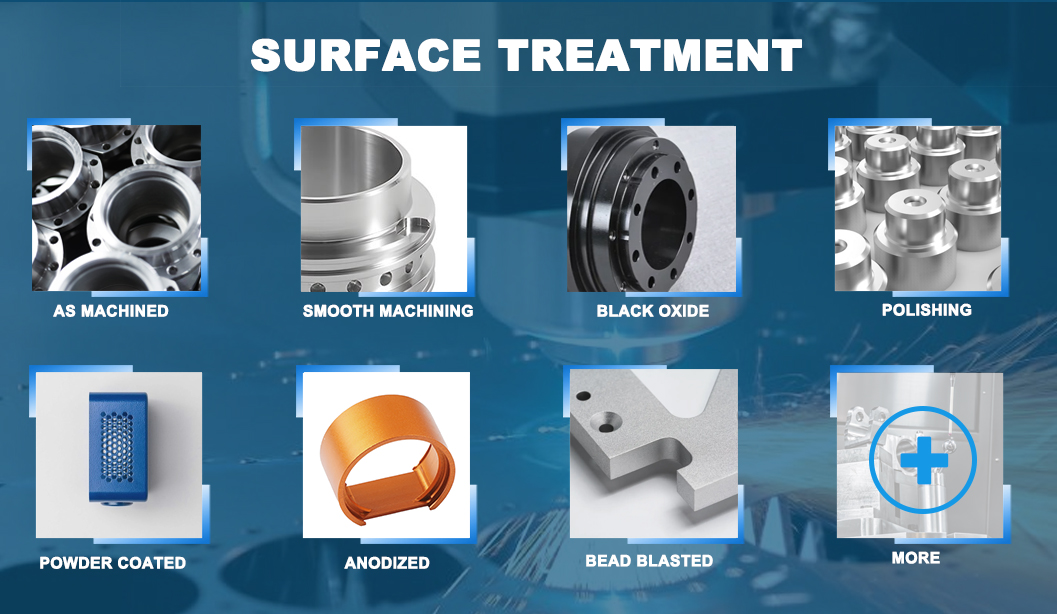
The surface finish of MIM parts can be improved by conventional processes such as grinding, lapping or burnishing.
Size of MIM Parts
There is, theoretically, no limit to the maximum size of part that could be produced, but economic considerations restrict the sizes that are currently viable.
There are two important factors in this connection:
The larger the part the greater is the proportion of the overall cost that is attributable to the raw material which is costly.
The total cost of the powder is a linear function of the weight of the part but in the case of parts produced by machining from solid bar stock, for example, the machining cost increase with increasing part size at a much lower rate.
The thicker the section the longer the debinding time, and thus the higher the cost of that part of the process.
At the present time, the limiting thickness seems to be about 30 mm.
A novel approach has been developed for a ‘binderless’ MIM process (4) whereby a homogeneous mixture of a powder and a liquid medium containing chemical additives is injected into a cold mould where the mixture is solidified.
After ejection from the mould the liquid (approx 1 wt% of the part) is evaporated in a vacuum a process which can take 1 to 2 days depending on part thickness, powder size and powder loading.
Fully dense parts up to 800 g have been made in this way with wall thicknesses greater than 20mm.